Plastic Recycling Pelletizing: How Plastic Scrap Becomes Pellets
The six steps from scrap to pellet, the three ways to cut pellets, when a two-stage machine is worth it, and what to keep out of the hopper.
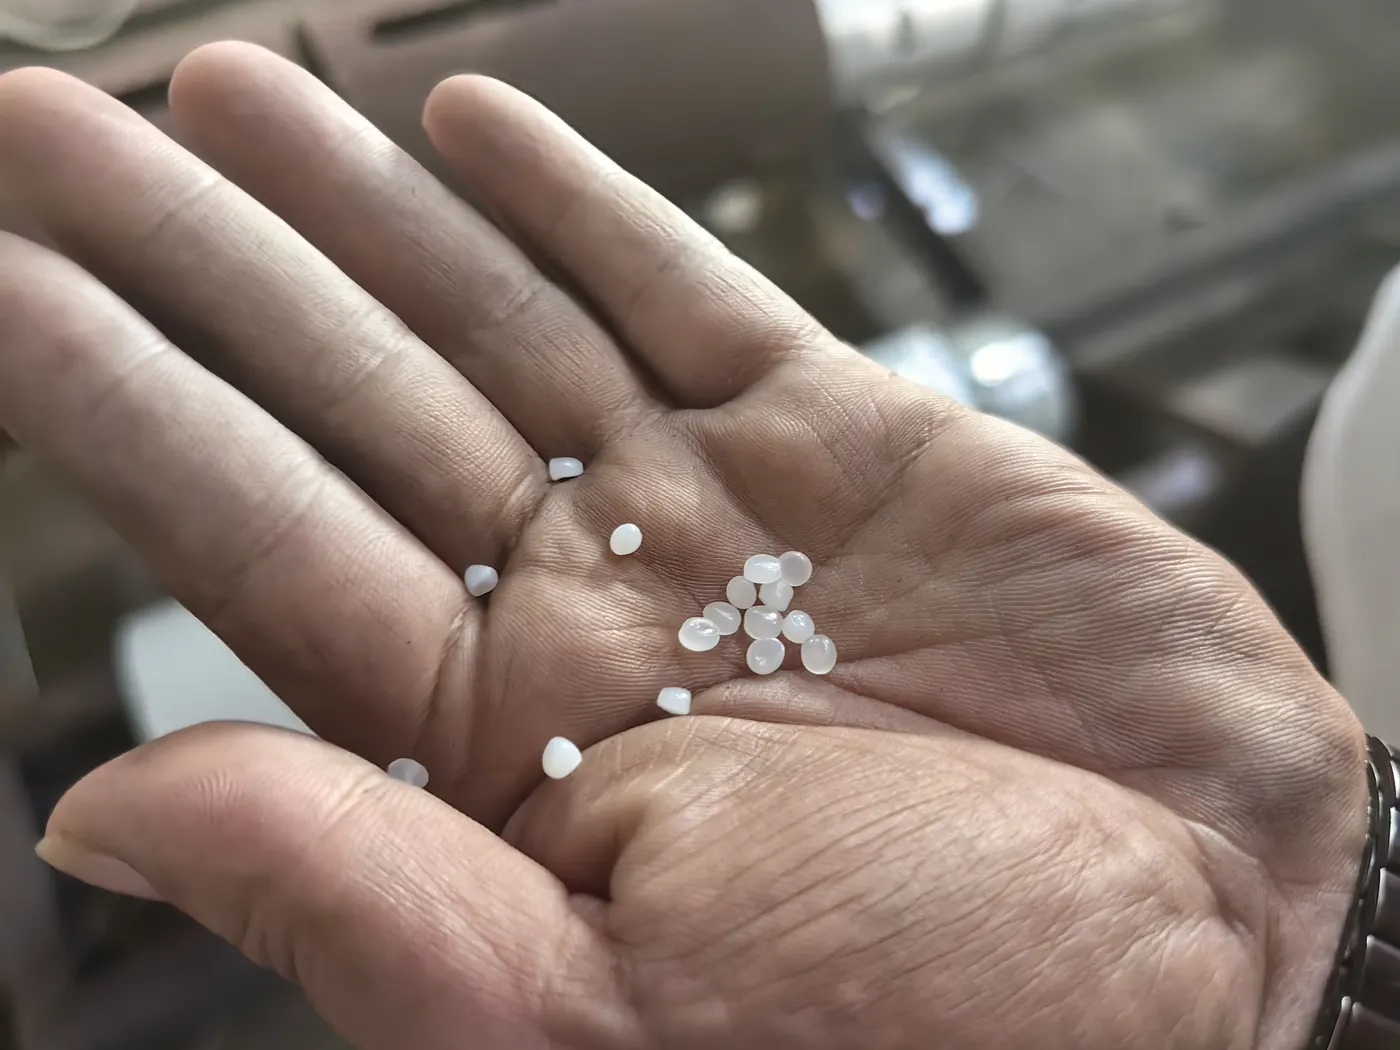
Plastic recycling pelletizing is the process of melting clean, sorted plastic scrap in an extruder, filtering the melt and cutting it into small, uniform pellets. The pellets can then be fed into a blown film machine or a molding machine much like new resin. Most recycled polyethylene and polypropylene goes through this step before it is used again.
This guide is for recyclers and for bag factories that want to reuse their own trim. We build pelletizers, blown film machines and bag making machines in Wenzhou, China, so the examples come from our plant. Where a point depends on your material, we say so.
The plastic pelletizing process in 6 steps
The plastic pelletizing process has six steps: sort, size-reduce, wash and dry, feed, melt and filter, then cut and cool. Clean factory trim can skip the first three. Post-consumer waste needs all of them.
1. Sort. Separate the scrap by polymer and, if the pellets must be light, by color. PE and PP look alike but do not mix well, and a few pieces of the wrong plastic can spoil a whole batch.
2. Shred. Rigid scrap such as crates and drums is cut into flakes in a shredder or a granulator. Film is cut into small pieces so it feeds evenly.
3. Wash and dry. Post-consumer film carries soil, labels and food residue, so it is washed and then dried. Water left in the material turns to steam in the extruder and leaves holes in the pellets.
4. Feed. Hard flakes drop into the hopper by gravity. Light film is harder to feed, so film machines use a feeder with an agitator, or a compactor, to push it into the screw.
5. Melt and filter. The screw melts the plastic, and a screen pack at the end of the barrel catches what did not melt: paper, sand, metal and other polymers. A screen changer lets the operator swap a blocked screen without a long stop.
6. Cut and cool. The filtered melt leaves the die as strands or is cut right at the die face. It is cooled in water, cut into pellets and dried before bagging.
Keep the blocked screens from the first week of production. Look at what is caught on them: paper fibers, sand or unmelted plastic. Each one points to a different fix upstream, and it costs nothing to check.
Strand, water-ring and underwater pelletizing
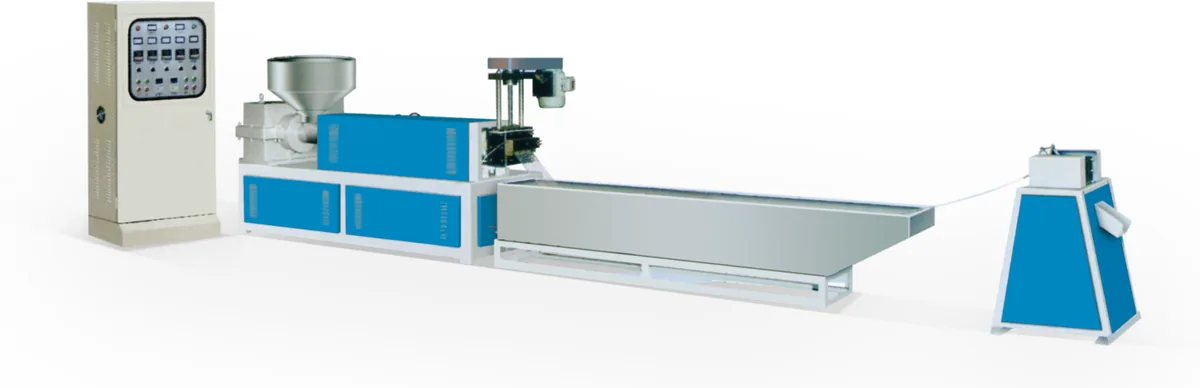
There are three common ways to cut pellets: strand, water-ring and underwater. Strand pelletizing is the simplest and the most common in film recycling. The other two cut at the die face and suit higher outputs or softer materials.
| Method | How it works | Typical pellet | Where it fits |
|---|---|---|---|
| Strand | Strands leave the die, cool in a water tank and are cut by a rotating cutter | Short cylinders | Most PE and PP recycling, small and mid-size plants. All our pelletizers work this way |
| Water-ring | A knife cuts at the die face and a ring of water carries the pellets away | Rounded discs | PE and PP at medium output, less floor space than a water tank |
| Underwater | The die face sits in a water chamber and the knife cuts under water | Round beads | High output and soft or sticky materials |
General descriptions. Recycled pellets are usually a few millimeters across, in the 2–5 mm range.
In plastic recycling pelletizing, strand lines are easy to watch and easy to fix. If a strand breaks, the operator sees it in the water tank and feeds it back into the cutter. The trade-off is floor space. The water tank on our single-stage machines takes much of their 4 to 6 meters of length.
Single-stage or two-stage: which do you need?
A single-stage pelletizer uses one extruder to melt and push the plastic. A two-stage pelletizer passes the melt from a main extruder into a second, auxiliary extruder before the die. Choose single-stage for clean, dense scrap. Choose two-stage for film and filament, and for higher output.
| Single-stage MF-B90 – MF-B120 | Two-stage MF-90 / MF-120 | |
|---|---|---|
| Extruders | 1 | 2 in series (main + auxiliary) |
| Best for | HDPE, LDPE and PP waste | PE and PP film and filament |
| Screw diameter | 90, 100, 110 or 120 mm | Main 95 or 120 mm, auxiliary 80 or 90 mm |
| Main motor | 22 to 45 kW | 22 or 30 kW, plus 7.5 or 11 kW auxiliary |
| Rated output | 70, 80, 90 or 100 kg/h | 150 or 200 kg/h |
| Weight | 2,600 to 3,200 kg | 1 to 1.5 t |
Manufacturer’s values for our two series. Actual output depends on the material, how clean it is and how it is fed.
The second extruder gives the melt a second chance. In two-stage designs in general, the break between the two screws is where trapped gas and moisture can escape, which helps with printed or slightly damp film. Our two-stage series is also rated higher: 150 or 200 kg/h, against 70 to 100 kg/h for the single-stage series.
If your scrap is mostly film thinner than 0.05 mm, ask the supplier to run a test with your own film, not with flakes. Thin film is light and bulky. Feeding it, not melting it, is usually what limits the output.
What should not go straight into a pelletizer
PVC, PET and other high-melting plastics, paper labels, dirt and water should be removed before pelletizing PE or PP. Each one causes a different problem, from blocked screens to holes in the pellets.
| In the scrap | What happens | What to do |
|---|---|---|
| PVC | Breaks down at PE processing temperatures and gives off corrosive gas, black specks in the pellets | Sort it out completely before shredding |
| PET, nylon | Melt far above PE, stay solid and block the screen | Sort out, or remove multi-layer film from the batch |
| Paper labels, dirt, sand | Screens block quickly, pellets look gray | Wash, use a finer screen, change screens more often |
| Water | Steam bubbles, hollow or foamy pellets | Dry the washed film before feeding |
| Heavy printing | Ink gives off gas, small holes, darker color | Expect darker pellets; a two-stage line handles printed film better |
| PE and PP mixed | Pellets run, but the film made from them is weaker | Pelletize PE and PP in separate batches |
Before you buy, send the supplier a photo of the scrap and a 1 kg bag of the real material. A photo shows the print, the labels and the dirt. The sample shows how the material feeds and how often the screen will need changing.
Recycling bag factory trim: a worked example
A bag factory can turn its own trim into pellets and feed them back to its blown film machine. Clean, single-polymer trim is the easiest material for plastic recycling pelletizing. It usually needs no washing at all.
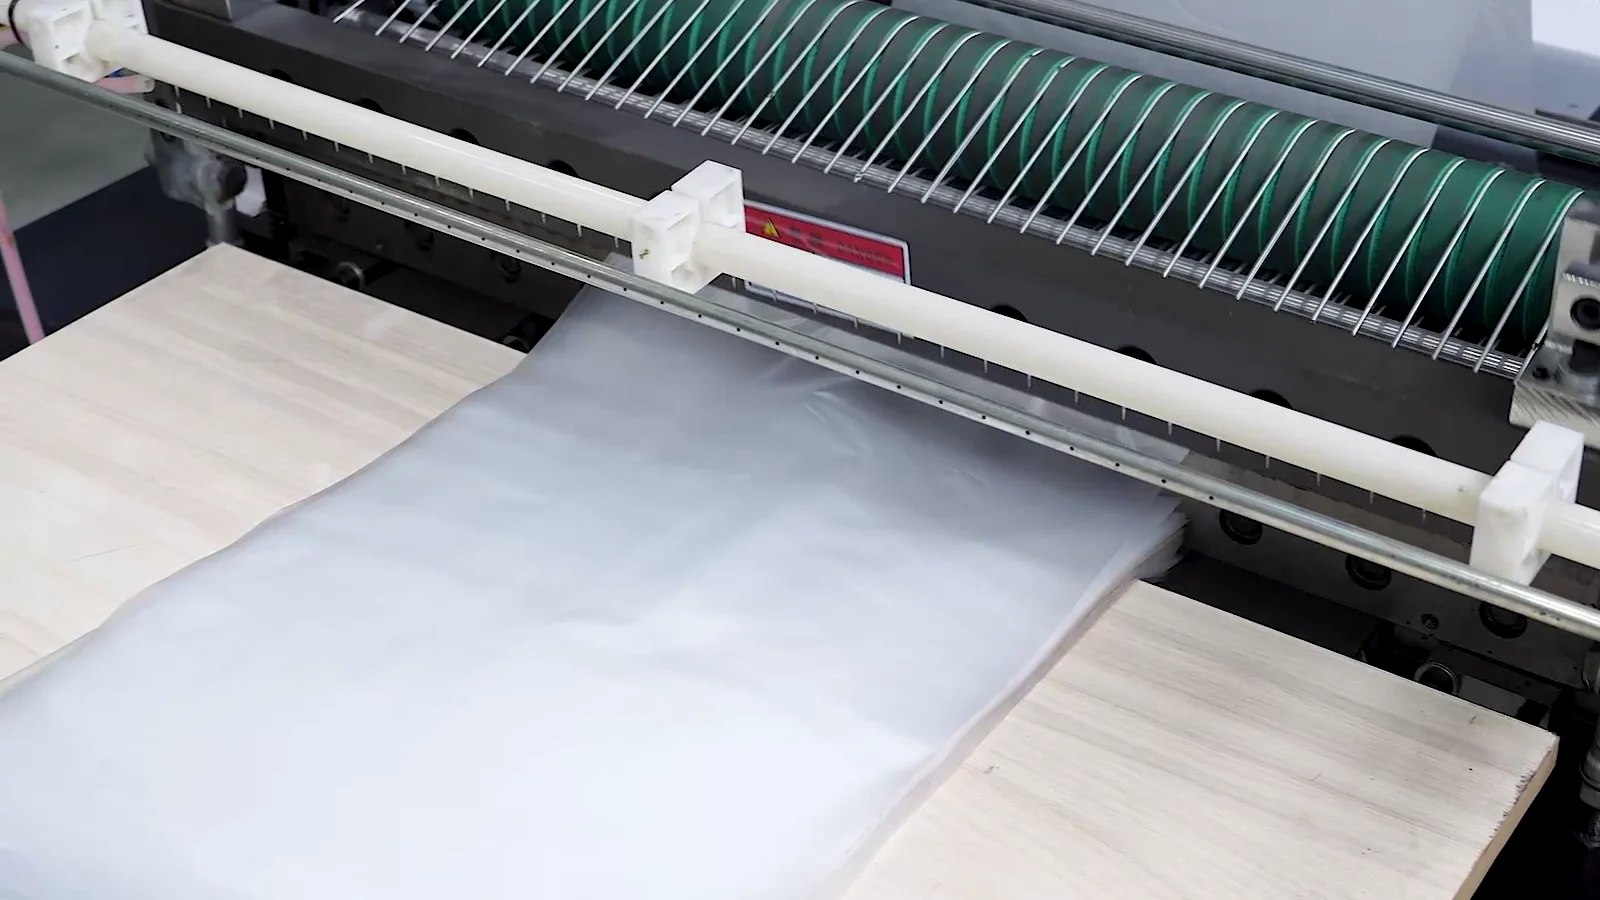
Here is how to size it. Weigh the trim from every shift for one week and take the daily average. Then divide by the rated output of the machine you are looking at, and add time for start-up and screen changes.
Say a factory collects 300 kg of clean HDPE trim a day. On a single-stage MF-B90 at 70 kg/h, that is a little over 4 hours of running. On an MF-B120 at 100 kg/h, it is about 3 hours. If the trim is bulky thin film that feeds slowly, the two-stage MF-90 at 150 kg/h would handle it in about 2 hours, and leave room for growth.
The pellets then go back into the extruder, blended with new resin. A trash bag accepts much more recycled content than a clear retail bag. Our guide on how plastic bags are made shows where the trim comes from and where the pellets go back in.
What drives plastic recycling pelletizing cost
Plastic recycling pelletizing cost per kilo depends mostly on energy, labor, screens and wear parts, and how clean the input is. The machine price matters less than people expect, because it is spread over every kilo the machine makes in its life.
| Cost item | What drives it | How to lower it |
|---|---|---|
| Energy | Motor and heater power, hours running, local electricity price | Run full batches, avoid long idle heating |
| Labor | Feeding by hand, watching strands, bagging | Keep the feed steady so less time is spent at the hopper |
| Screens and wear parts | Dirt in the scrap, screw and cutter wear | Cleaner input, regular checks of the cutter blades |
| Washing and drying | Only for dirty post-consumer scrap | Collect trim clean at the bag machine |
| Machine | Price spread over years of output | Size the machine to your real daily volume |
Compare the result with what the scrap is worth today. Many factories sell trim cheaply as waste and buy resin at full price. Pelletizing closes that gap, but only if the pellets are clean enough for the bags you make.
During the factory test, ask for the main motor current and the output in kilos per hour with your own material. Those two numbers let you estimate kWh per kilo for your plant. A rated output on paper does not.
Our pelletizers for PE and PP recycling
We build two pelletizer series for plastic recycling pelletizing, both with strand cutting and water cooling. The single-stage MF-B series has four sizes from 70 to 100 kg/h for HDPE, LDPE and PP waste, with a motor-driven screen changer and a cutter synchronized with the extruder. The two-stage MF-90 and MF-120 make 150 or 200 kg/h of pellets from PE and PP film and filament.
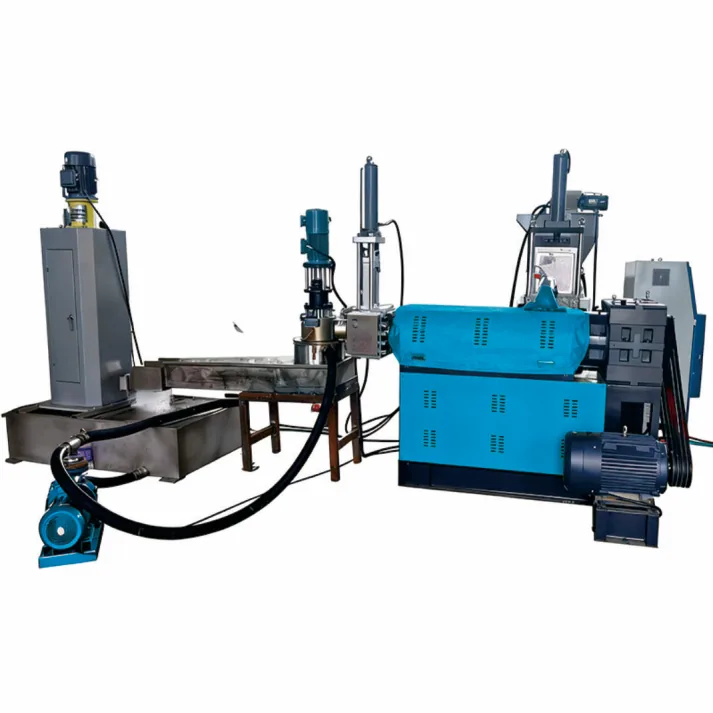
Our pelletizers cover steps 4 to 6. Shredding and washing need separate equipment, and not every scrap is worth pelletizing. If yours is mixed, very dirty or multi-layer, we will tell you before you buy. Each machine comes with a 12-month warranty (wear parts excluded) and remote video support for start-up. Compare both series on the plastic pelletizing machine page.
Frequently asked questions
How is plastic recycled into pellets?
Plastic is recycled into pellets in six steps: sorting, shredding, washing and drying, feeding into an extruder, melting and filtering through a screen, then cutting and cooling. The filtered melt leaves the die as strands, cools in water and is cut into pellets a few millimeters long. Clean factory trim can skip sorting and washing.
What are recycled plastic pellets?
Recycled plastic pellets are small, uniform granules made by melting and filtering plastic scrap. They replace part of the new resin in film, bags, pipes and molded parts. Their quality depends on how clean and well sorted the scrap was, so pellets from clean factory trim are usually better than pellets from mixed post-consumer waste.
What is the use of recycled plastic pellets?
Recycled PE and PP pellets go back into blown film for trash bags and other bags, and into injection molding, pipes and plastic lumber. Bag factories often blend them with new resin in the extruder. The share depends on the product: a black trash bag accepts much more recycled content than a clear retail bag.
How much does plastic recycling pelletizing cost?
The cost per kilo depends on electricity, labor, screens and wear parts, washing if the scrap is dirty, and the machine price spread over its working life. Clean bag factory trim is the cheapest to pelletize because it needs no washing. Measure the motor current and output on your own material during a test to estimate energy per kilo.
How much does a plastic pelletizing machine cost?
The price depends on the number of extruders, screw size, output, the screen changer and the cutting method, and on whether a shredder, washer or dryer is included. A single-stage machine usually costs less than a two-stage machine of similar size. Ask for a quotation based on your material and daily volume, so the machine is not oversized.
What is a plastic granulator?
In recycling, a plastic granulator usually means a cutting mill that grinds rigid scrap into small flakes, called regrind. It does not melt the plastic. Some suppliers also call pelletizers granulating machines, because the product is granules. If a quotation says granulator, check whether it melts and filters the plastic or only cuts it.
Further reading on the wider picture: the Wikipedia article on plastic recycling. For the extruder itself, see our guide to the types of extruders. Not sure which pelletizer fits your scrap? Send us a photo with the material and kilos per day, and we will reply within 24 hours.