How Plastic Bags Are Made: The Process Step by Step
From polyethylene resin to the finished bag: what happens on each machine in a bag factory, with photos and videos from our plant.
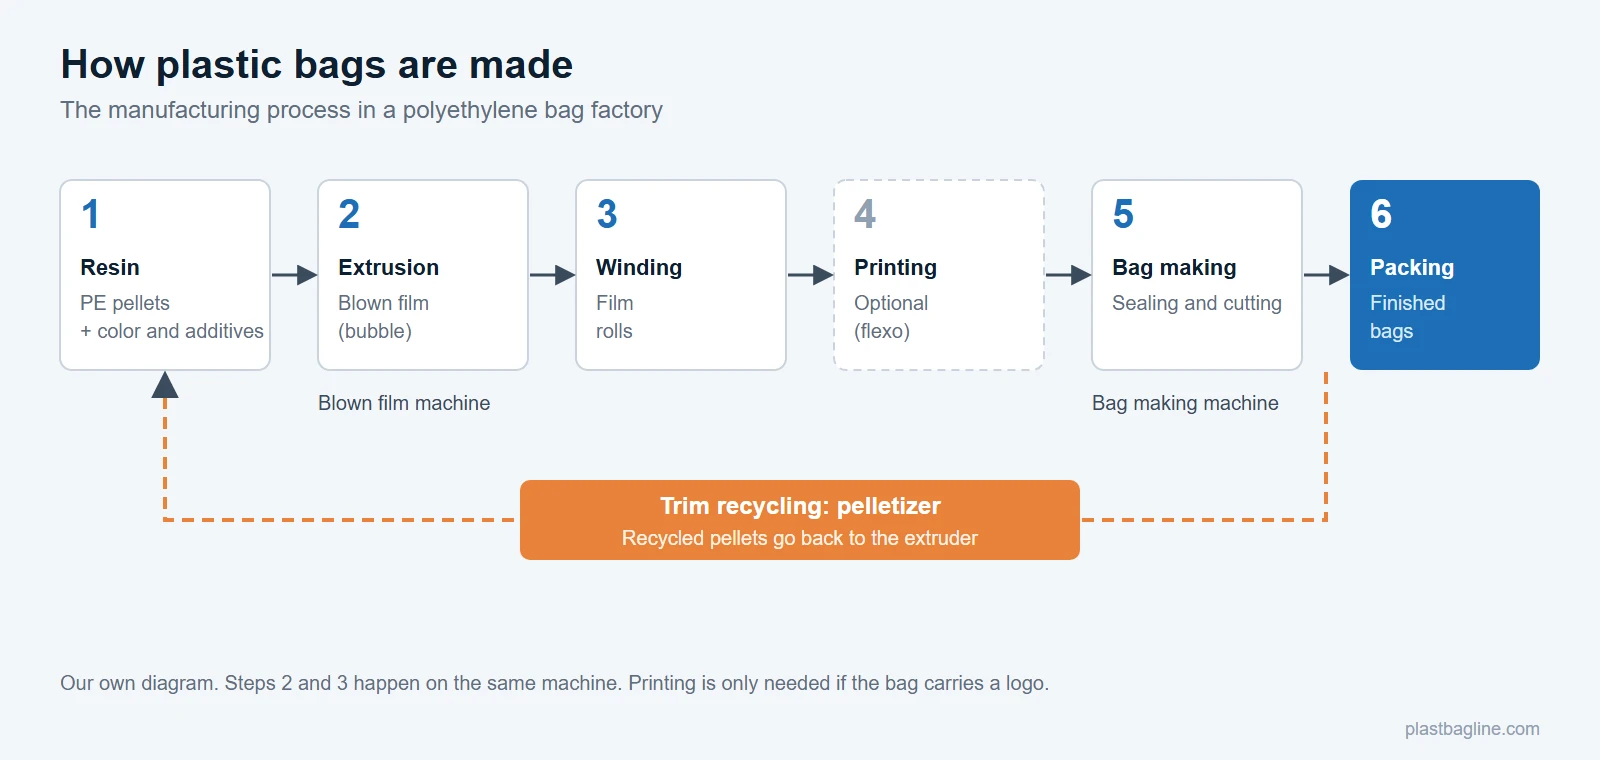
Plastic bags are made on two main machines. A blown film extruder melts polyethylene pellets and forms a thin film as a bubble, and a bag making machine seals and cuts that film into bags. In between, the film is wound into rolls and, if the bag carries a logo, printed.
In this guide we explain how plastic bags are made step by step, with photos and videos from our plant in Wenzhou, China. We build blown film machines, bag making machines and pelletizers, so we describe the process from inside the factory.
What are plastic bags made of?
Almost all plastic bags are made of polyethylene, a plastic made from ethylene. Three types are used. High-density polyethylene (HDPE) makes thin, strong bags such as the T-shirt bag, low-density polyethylene (LDPE) makes soft, clear bags, and linear low-density polyethylene (LLDPE) is blended in for stretch.
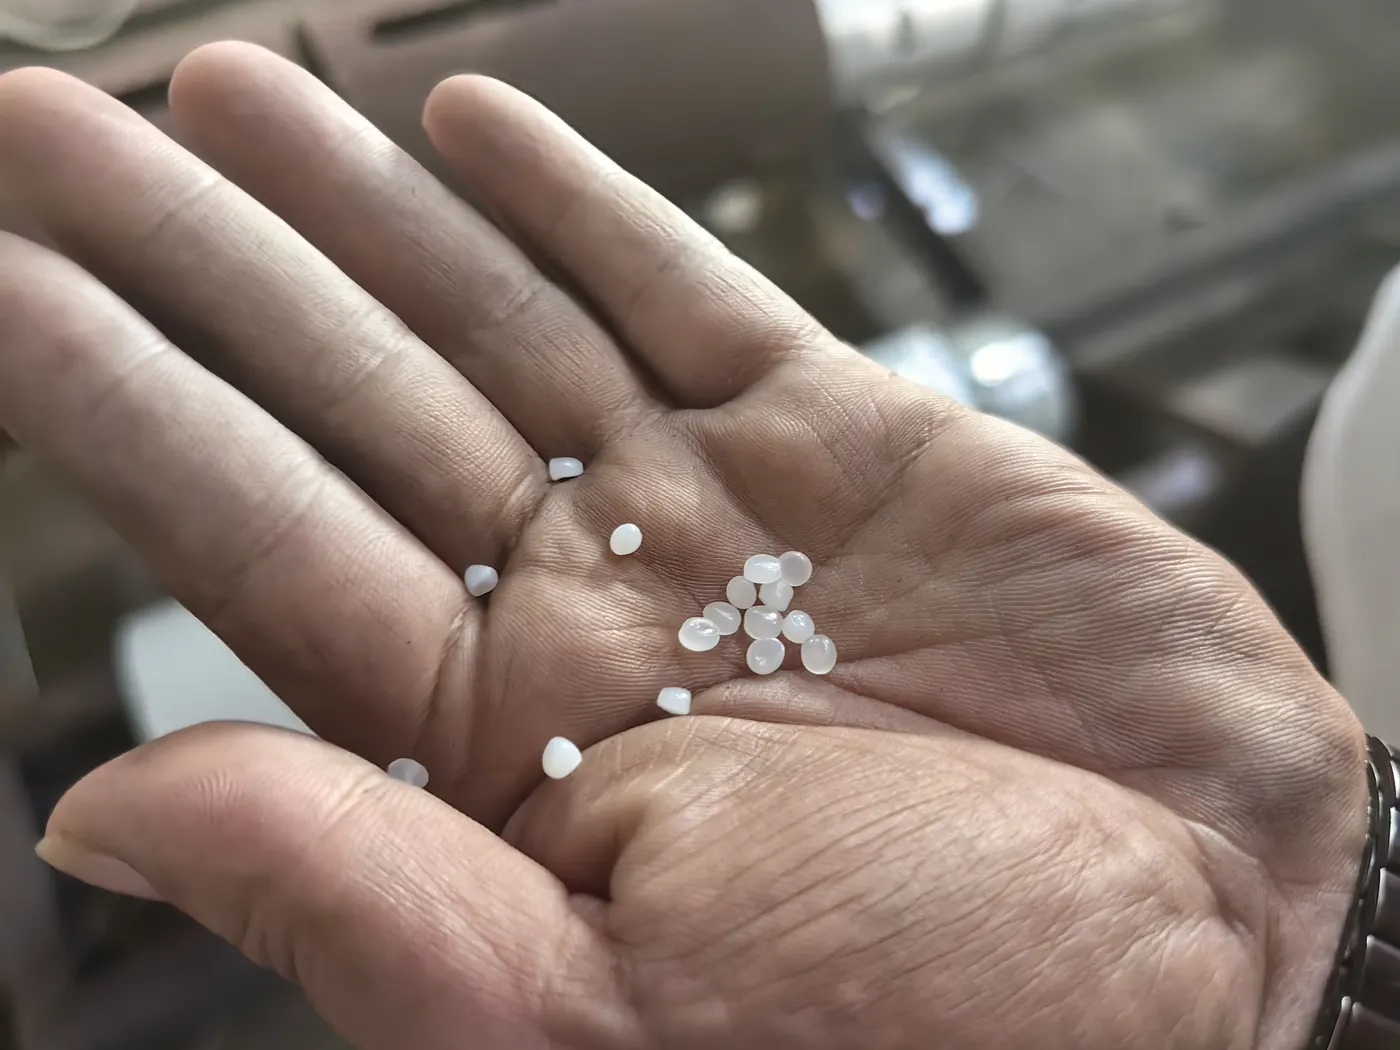
The resin arrives at the factory as pellets about the size of a lentil. Color concentrate (masterbatch) and additives can be added to it. Our article on HDPE vs LDPE compares the two materials and which one suits each bag.
Step 1: preparing the resin
To understand how plastic bags are made, start with the blend. The first step is to mix the resin with color and additives in the ratio the bag requires. The blend goes into the extruder hopper, often through an automatic vacuum loader.
If the factory recycles its own trim, some recycled pellets are added at this step. How much depends on the film: a trash bag accepts more recycled content than a clear retail bag.
Step 2: blown film extrusion
In the extruder, a screw inside a heated barrel melts the resin and pushes it into a circular die. The plastic leaves the die as a thin tube, and air blown in through the center inflates it into a bubble. When the film comes out wrong, see our blown film troubleshooting guide.
An air ring cools the bubble as it rises through the tower. The bubble diameter sets the film width, and the haul-off speed sets the thickness. Our mini blown film machine produces 40 to 50 kg of film per hour, and the MF-C series reaches 220 kg/h.
If the bag will be printed, the film needs corona treatment before printing, because ink does not stick to untreated polyethylene. On our blown film machines corona treatment is an option: ask for it with the quote, because it mounts on the upper part of the line.
Step 3: flattening and winding
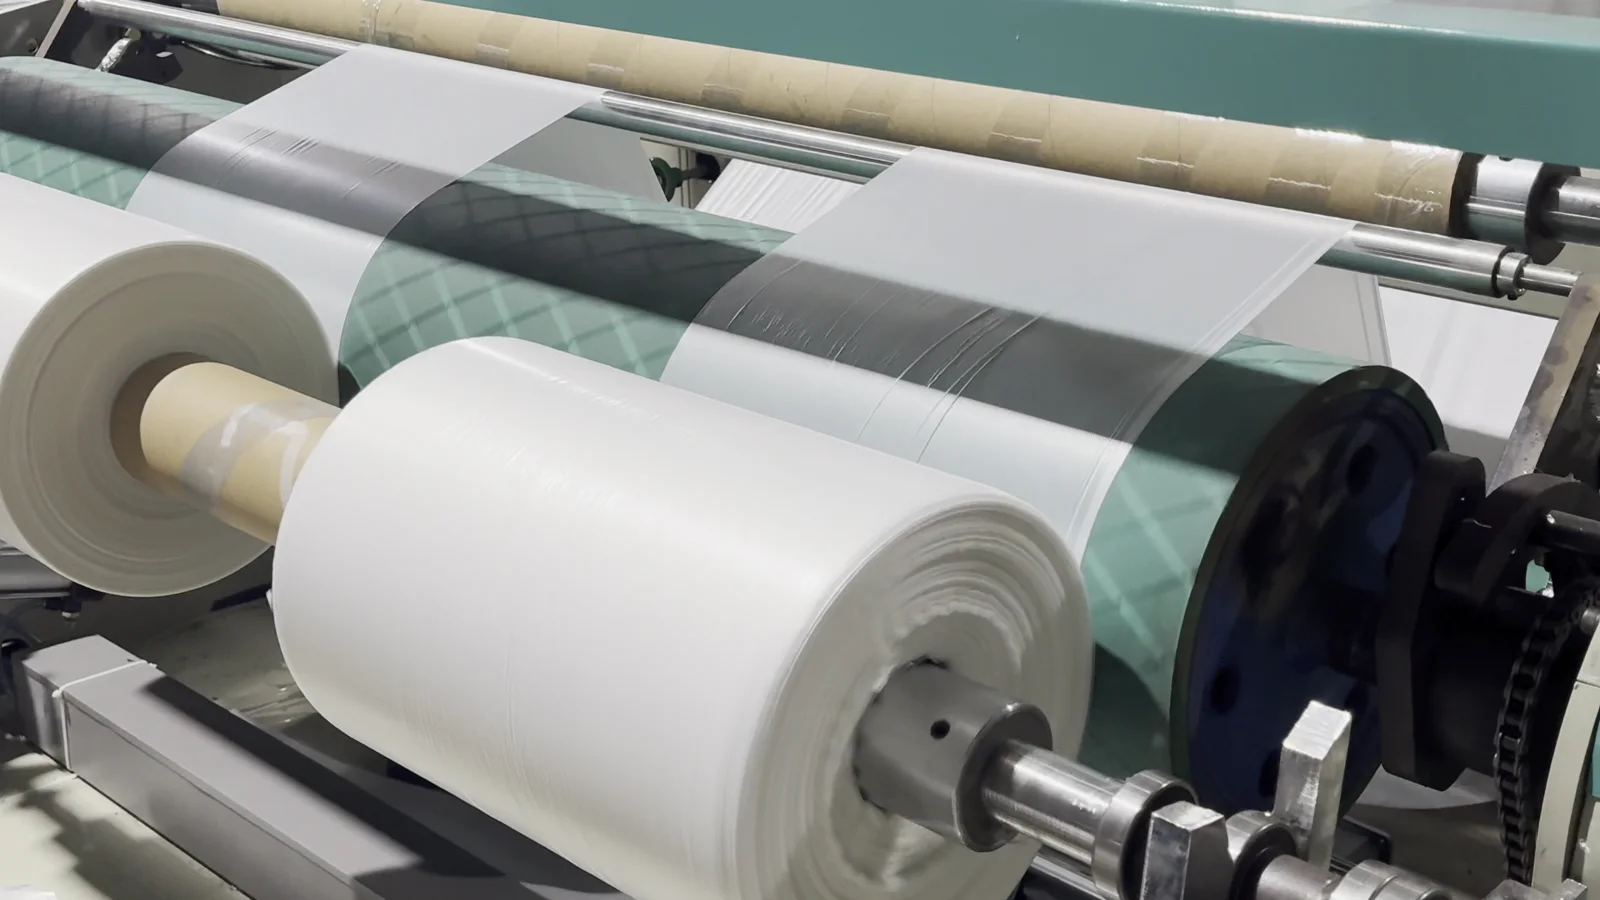
At the top of the tower, nip rollers flatten the bubble into a double layer of film. The film then runs down to the winder, which rolls it up for the next machine.
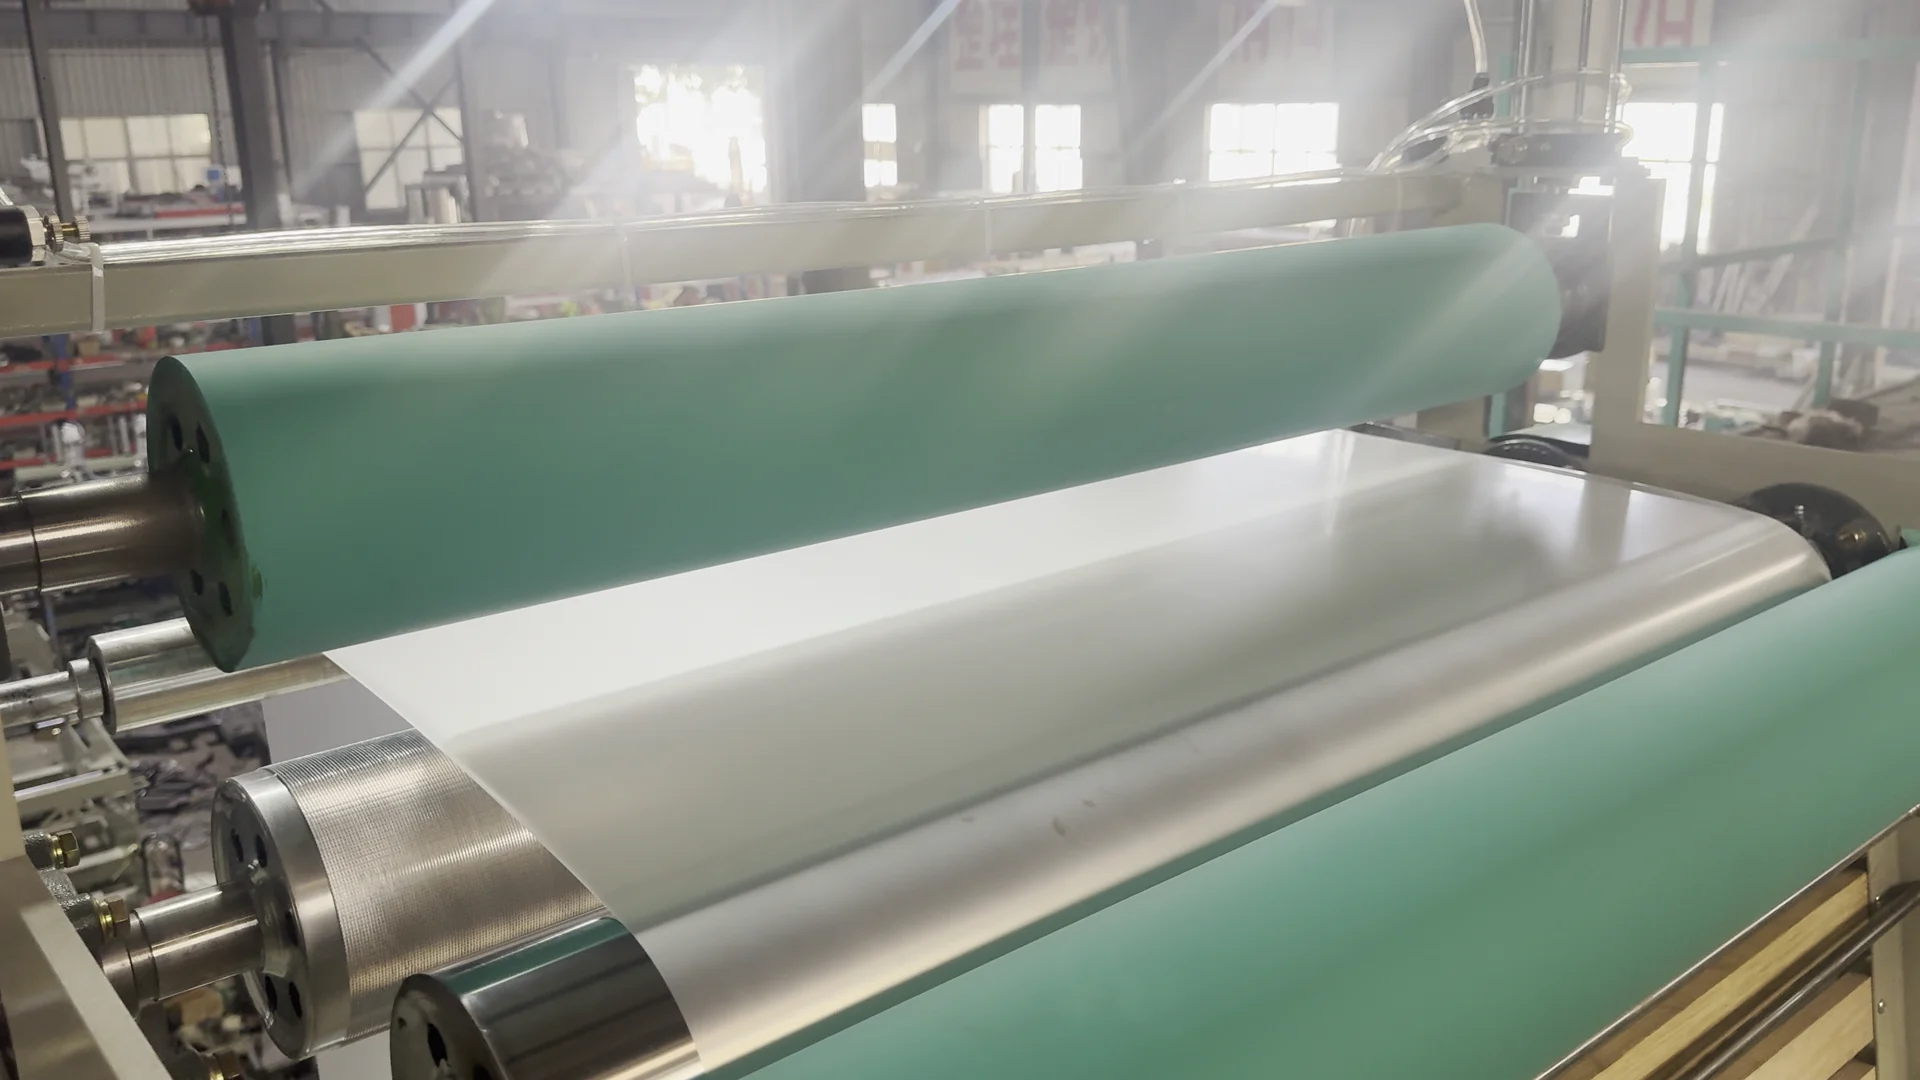
Depending on the bag, the film can come off as a closed tube, with side gussets for T-shirt bags, or slit into two sheets. Each roll is weighed and labeled so the plant knows how many bags it will yield.
Step 4 (optional): printing
If the bag carries a logo or text, the roll goes through a printing press before the bag machine. For polyethylene bags the most common method is flexographic printing, which prints roll to roll.
Many small factories start without a press and sell plain bags, or send rolls out for printing. Our bag lines do not include printing presses, so we do not cover printing in detail here.
Step 5: sealing and cutting on the bag machine
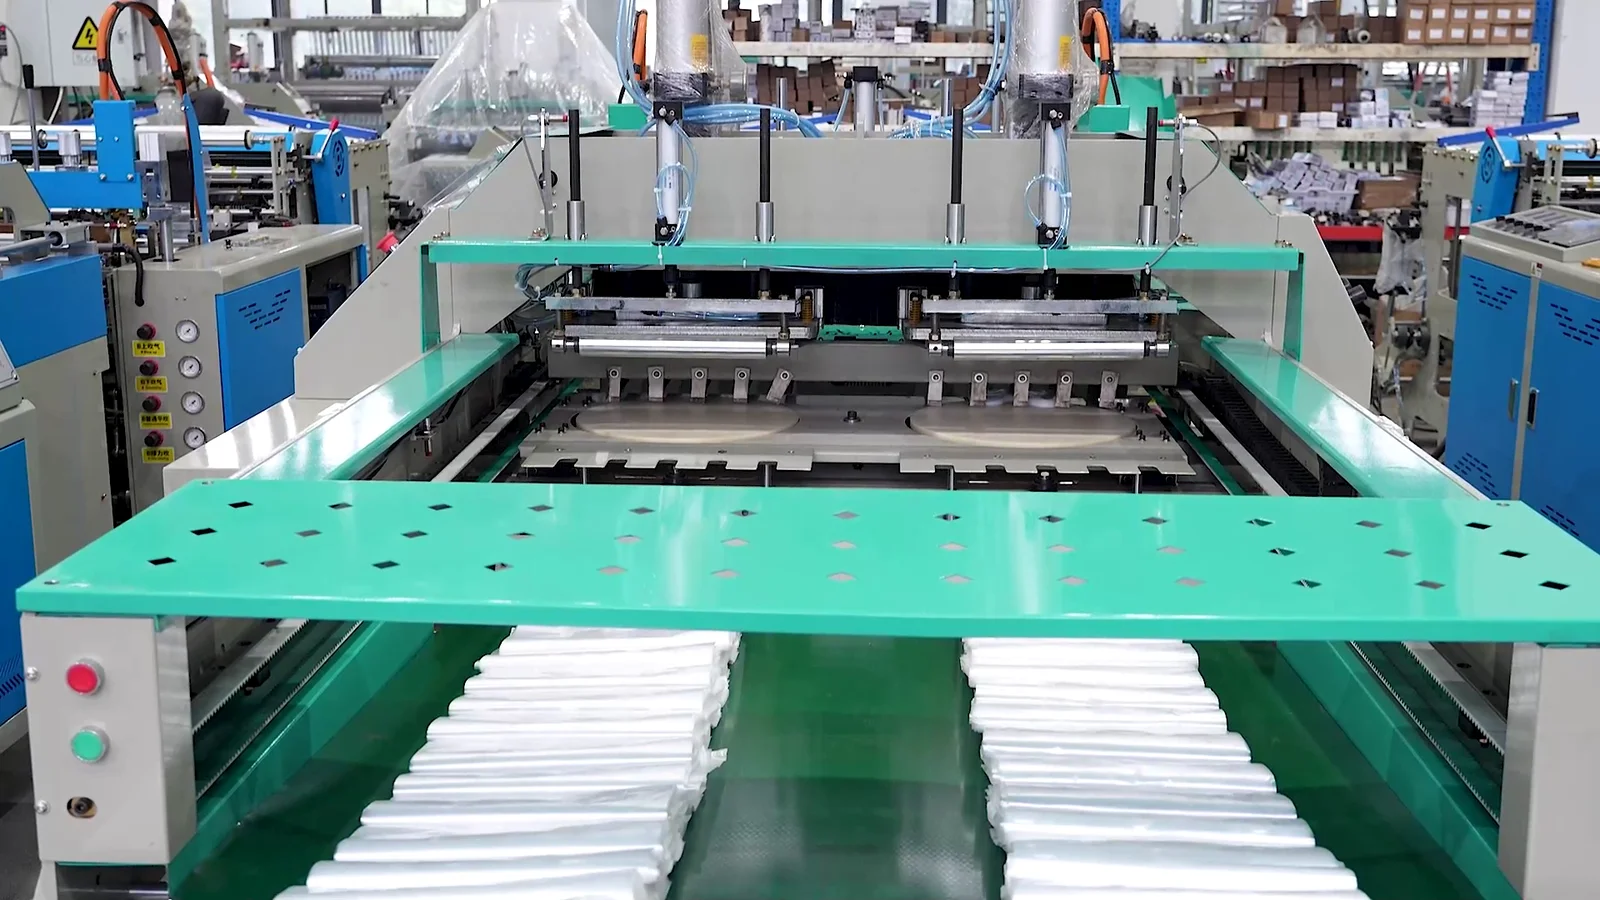
The bag making machine takes the film roll, heat-seals it and cuts it into individual bags. The sealing and cutting method depends on the bag, which is why each bag type has its own machine.
| Bag | How it is sealed and cut | Our machine | Speed |
|---|---|---|---|
| T-shirt bag | Bottom seal, hot cut, handles punched out | MFHQB | Up to 350 bags/min per line, 2 lines |
| Bags on a roll and trash bags | Bottom seal and perforation between bags, then wound | YB400 | 20–250 bags/min per line, 2 lines |
| Mailer bag | Side seals, with a flap for closing | MF-600B / 800B / 1000B | 40–240 bags/min |
| Flat bag | Sealed first, then cold cut | MF-B | 50–120 bags/min per line, 2 lines |
Catalog speeds. Real speed depends on bag length and thickness.
When you compare bag machines, do not compare only the maximum speed. Ask how many bags per minute the machine runs at your bag length and thickness. A longer bag always runs slower than the short bag used to measure the maximum.
Step 6: packing and recycling the trim
Finished bags are counted, bundled and packed into cartons or sacks. Bags on a roll come off already wound and only need packing. That completes how plastic bags are made in a factory.
The bag machine always leaves trim: the cut-out handles, the edges and the set-up bags at start-up. That trim can go through a pelletizer and back into the extruder as pellets, instead of being sold as waste. Our guide to plastic recycling pelletizing walks through each step.
Weigh the trim from each shift for a week before deciding on a pelletizer. Our smallest pelletizer, the MF-B90 single-stage, processes 70 kg/h. With your trim weight you will know how many hours a day it would run.
How are trash bags made?
Trash bags are made the same way as other plastic bags: the film is extruded and then sealed on a bag machine. The difference is the bag machine, which perforates the film between bags without separating them and winds the result into a roll, like our YB400.
Because a trash bag does not need to be clear, it is usually black or green and contains some recycled material. That makes it the natural place for the factory’s own recycled pellets.
If you make trash bags with recycled pellets, test the blend on the extruder at a low percentage first and raise it step by step. The practical limit depends on how clean your trim is.
How plastic bags are made: frequently asked questions
How are plastic bags made step by step?
Resin pellets are mixed with color and additives, melted in a blown film extruder and blown into a thin film bubble. The bubble is flattened and wound into rolls. If needed, the film is printed. A bag machine then heat-seals and cuts it into bags, which are counted and packed. Trim is recycled into pellets.
What is the raw material of plastic bags?
The raw material is polyethylene resin in pellet form. Polyethylene is made from ethylene, a gas produced from natural gas or crude oil. The bag factory buys the resin as pellets and melts it in the extruder.
How is polyethylene made?
Ethylene gas, produced by cracking natural gas liquids or oil fractions, is polymerized in a reactor so that its molecules link into long chains. Depending on the process, pressure and catalyst, the result is HDPE, LDPE or LLDPE, which the resin plant cuts into pellets.
What are the properties of a plastic bag?
A polyethylene bag is light, waterproof, flexible and strong for its weight, and it can be heat-sealed. HDPE bags are thin, stiff and crinkly. LDPE bags are soft, clear and stretchy. Thickness, usually measured in microns or mils, sets how much weight the bag can carry.
How are plastic bags recycled?
Collected bags are sorted, shredded, washed and dried, then melted in a recycling extruder and cut into pellets. The pellets are used in new film, trash bags or other products. In a bag factory, clean trim skips the washing step and can go straight to the pelletizer.
Why are potato chip bags not recyclable?
Most chip bags are laminates of several plastics, often with a thin metallized layer, bonded together. Because the layers cannot be separated easily, the bag does not fit into the single-material recycling streams used for polyethylene bags.
To see which machines you need for the bag you want to sell, visit the plastic bag production line page or read our guide to types of extruders. For background on the product itself, see the Wikipedia article on plastic bags. If you are weighing paper bags instead, this overview of types of paper bag making machines covers the other side. Questions? Write to us and we will reply within 24 hours.